Cleanroom solutions and research
CLEANROOM PRODUCTS
 Controlled Expansion Of Supercritical Solutions (CESS®) Technology
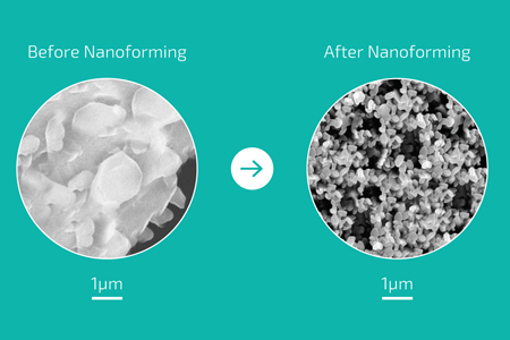
Nanoform’s award-winning Controlled Expansion of Supercritical Solutions (CESS®) technology is a bottom-up nanoparticle engineering approach that enables the creation of API nanoparticles and can unlock the full therapeutic potential of small molecule drugs.
-
 Primary Pharmaceutical Glass Packaging
We’ve applied our expertise in glass science, optical physics, vapor deposition, precision forming, and extrusion to design and develop a 21st century glass container to protect 21st century drugs and vaccines. Corning® Valor® Glass vials enhance the storage and delivery of drugs, providing more reliable access to medicines essential to public health.
-
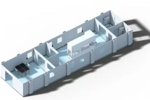
 Faciliflex Cleanroom Module For Drug Manufacturing
Faciliflex Module offers the ultimate flexibility in cleanroom design—pre-configured, modular “base blocks” that allow you to mix-and-match all the components you need for your next cleanroom facility.
-
 Pharmaceutical Net Pro: Environmental Monitoring Software
Viable, Non Viable and Environmental Monitoring Software.
-
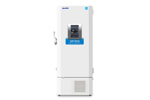
 Obtain Temperature Uniformity With An Ultra-Low Temperature Freezer
PHCbi brand's 18.6 cu.ft (528L) ultra-low temperature freezer operates on 220V and features VIP Plus vacuum insulated panels to deliver reliable temperature uniformity throughout the chamber. ENERGY STAR® Certified.
-
 AeroTrak™+ Portable Particle Counter A100 Series
Flow Rate 1 CFM (28.3 LPM) - 3.5 CFM (100 LPM) / Channel Sizes 0.3 µm to 10 µm,(6) user selectable channels.
-
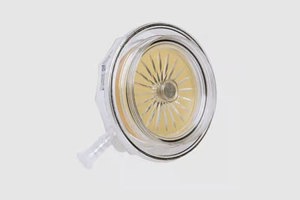
 Sterile Filtration Of Cell Debris
AccuStrain™ 40μm & 150μm Filters are designed and packaged for bioprocessing applications, providing filtration of cell aggregates and extraneous particulate removal in cell separation, media preparation, and final fill workflows.
-
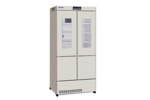
 Pharmaceutical Refrigerator Freezer Combo
PHCbi brand's 14.7 cu.ft (415L) refrigerator and 6.2 cu.ft (176L) freezer combination unit is designed for temperature performance not commonly found in commercial cabinets. It combines high performance refrigeration control and monitoring systems with energy efficient and cost-effective cabinet design. Separate refrigeration systems and compressors allow you to maintain proper temperature uniformity while saving space for even the smallest of facilities.
-
 Custom API Manufacturing From Early Development To Commercial
At Siegfried, we combine scientific expertise with a global manufacturing network to deliver reliable, high-quality custom APIs for innovative medicines, from early development to commercial scale.
-
 Setting The New Standard For Aseptic Processing: Esco OxAP Isolator
Advanced positive-pressure isolators with integrated nebulized decontamination protect sensitive cell processing and aseptic filling operations while ensuring strict cGMP compliance.
-
 Glass Vial Forming Lines
Stevanato Group vial forming lines come in a variety of specifications that vary depending on the production requirements. By maintaining close ties with the customer throughout every step of the process, we can design and manufacture fully tailored, purpose-built equipment capable of producing vials with entirely custom dimensions and shape.




CLEANROOM OVERVIEW
Cleanrooms can be very large. Entire manufacturing facilities can be contained within a cleanroom with factory floors covering thousands of square meters. They are used extensively in semiconductor manufacturing, biotechnology, the life sciences and other fields that are very sensitive to environmental contamination.
The air entering a cleanroom from outside is filtered to exclude dust, and the air inside is constantly recirculated through high-efficiency particulate air (HEPA) and/or ultra-low penetration air (ULPA) filters to remove internally generated contaminants.
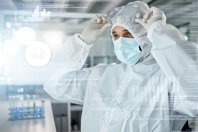
Staff enter and leave through airlocks (sometimes including an air shower stage), and wear protective clothing such as hoods, face masks, gloves, boots and coveralls.
Equipment inside the cleanroom is designed to generate minimal air contamination. Only special mops and buckets are used. Cleanroom furniture is designed to produce a minimum of particles and to be easy to clean.
Common materials such as paper, pencils, and fabrics made from natural fibers are often excluded, and alternatives used. Cleanrooms are not sterile (i.e., free of uncontrolled microbes);[3] only airborne particles are controlled. Particle levels are usually tested using a particle counter and microorganisms detected and counted through environmental monitoring methods.[4][5]
Some cleanrooms are kept at a positive pressure so that if there are any leaks, air leaks out of the chamber instead of unfiltered air coming in.
Some cleanroom HVAC systems control the humidity to low levels, such that extra equipment ("ionizers") is necessary to prevent electrostatic discharge (ESD) problems.
Low-level cleanrooms may only require special shoes, with completely smooth soles that do not track in dust or dirt. However, for safety reasons, shoe soles must not create slipping hazards. Access to a cleanroom is usually restricted to those wearing a cleanroom suit.[6]
In cleanrooms in which the standards of air contamination are less rigorous, the entrance to the cleanroom may not have an air shower. There is an anteroom (known as a "gray room"), in which clean-room clothing must be put on, from which a person can walk directly into the room (as seen in the photograph on the right).
Some manufacturing facilities do not use fully classified cleanrooms, but use some cleanroom practices to maintain their contamination requirements.[7][8]
Air flow principles

|

|
Cleanrooms maintain particulate-free air through the use of either HEPA or ULPA filters employing laminar or turbulent air flow principles. Laminar, or unidirectional, air flow systems direct filtered air downward in a constant stream towards filters located on walls near the cleanroom floor or through raised perforated floor panels to be recirculated. Laminar air flow systems are typically employed across 80 percent of a cleanroom ceiling to maintain constant air processing. Stainless steel or other non-shed materials are used to construct laminar air flow filters and hoods to prevent excess particles entering the air. Turbulent, or non-unidirectional, air flow uses both laminar air flow hoods and non-specific velocity filters to keep air in a cleanroom in constant motion, although not all in the same direction. The rough air seeks to trap particles that may be in the air and drive them towards the floor, where they enter filters and leave the cleanroom environment.[9]
Cleanroom classifications
Cleanrooms are classified according to the number and size of particles permitted per volume of air. Large numbers like "class 100" or "class 1000" refer to FED-STD-209E, and denote the number of particles of size 0.5 µm or larger permitted per cubic foot of air. The standard also allows interpolation, so it is possible to describe, for example, "class 2000".
A discrete-particle-counting, light-scattering instrument is used to determine the concentration of airborne particles, equal to and larger than the specified sizes, at designated sampling locations.
Small numbers refer to ISO 14644-1 standards, which specify the decimal logarithm of the number of particles 0.1 µm or larger permitted per cubic metre of air. So, for example, an ISO class 5 cleanroom has at most 105 = 100,000 particles per cubic metre.
Both FS 209E and ISO 14644-1 assume log-log relationships between particle size and particle concentration. For that reason, zero particle concentration does not exist. The table locations without entries are non-applicable combinations of particle sizes and cleanliness classes, and should not be read as zero.
Because 1 m3 is approximately 35 ft3, the two standards are mostly equivalent when measuring 0.5 µm particles, although the testing standards differ. Ordinary room air is approximately class 1,000,000 or ISO 9.[10]
US FED STD 209E cleanroom standards
| Class | maximum particles/ft3 |
ISO equivalent |
||||
|---|---|---|---|---|---|---|
| ≥0.1 µm | ≥0.2 µm | ≥0.3 µm | ≥0.5 µm | ≥5 µm | ||
| 1 | 35 | 7.5 | 3 | 1 | 0.007 | ISO 3 |
| 10 | 350 | 75 | 30 | 10 | 0.07 | ISO 4 |
| 100 | 3,500 | 750 | 300 | 100 | 0.7 | ISO 5 |
| 1,000 | 35,000 | 7,500 | 3000 | 1,000 | 7 | ISO 6 |
| 10,000 | 350,000 | 75,000 | 30,000 | 10,000 | 70 | ISO 7 |
| 100,000 | 3.5×10⁶ | 750,000 | 300,000 | 100,000 | 700 | ISO 8 |
US FED STD 209E was officially cancelled by the General Services Administration of the US Department of Commerce November 29, 2001,[11][12] but is still widely used.
ISO 14644-1 cleanroom standards
| Class | maximum particles/m3 |
FED STD 209E equivalent |
|||||
|---|---|---|---|---|---|---|---|
| ≥0.1 µm | ≥0.2 µm | ≥0.3 µm | ≥0.5 µm | ≥1 µm | ≥5 µm | ||
| ISO 1 | 10 | 2.37 | 1.02 | 0.35 | 0.083 | 0.0029 | |
| ISO 2 | 100 | 23.7 | 10.2 | 3.5 | 0.83 | 0.029 | |
| ISO 3 | 1,000 | 237 | 102 | 35 | 8.3 | 0.29 | Class 1 |
| ISO 4 | 10,000 | 2,370 | 1,020 | 352 | 83 | 2.9 | Class 10 |
| ISO 5 | 100,000 | 23,700 | 10,200 | 3,520 | 832 | 29 | Class 100 |
| ISO 6 | 1.0×10⁶ | 237,000 | 102,000 | 35,200 | 8,320 | 293 | Class 1,000 |
| ISO 7 | 1.0×10⁷ | 2.37×10⁶ | 1,020,000 | 352,000 | 83,200 | 2,930 | Class 10,000 |
| ISO 8 | 1.0×10⁸ | 2.37×10⁷ | 1.02×10⁷ | 3,520,000 | 832,000 | 29,300 | Class 100,000 |
| ISO 9 | 1.0×10⁹ | 2.37×10⁸ | 1.02×10⁸ | 35,200,000 | 8,320,000 | 293,000 | Room air |
BS 5295 cleanroom standards
| maximum particles/m3 | ||||||
| Class | ≥0.5 µm | ≥1 µm | ≥5 µm | ≥10 µm | ≥25 µm | |
|---|---|---|---|---|---|---|
| Class 1 | 3,000 | 0 | 0 | 0 | ||
| Class 2 | 300,000 | 2,000 | 30 | |||
| Class 3 | 1,000,000 | 20,000 | 4,000 | 300 | ||
| Class 4 | 200,000 | 40,000 | 4,000 | |||
BS 5295 Class 1 also requires that the greatest particle present in any sample does not exceed 5 μm.[13]
GMP EU classification
| Class | maximum particles/m3[14] | |||
|---|---|---|---|---|
| At Rest | At Rest | In Operation | In Operation | |
| 0.5 µm | 5 µm | 0.5 µm | 5 µm | |
| Class A | 3,520 | 20 | 3,520 | 20 |
| Class B | 3,520 | 29 | 352,000 | 2,900 |
| Class C | 352,000 | 2,900 | 3,520,000 | 29,000 |
| Class D | 3,520,000 | 29,000 | n/a | n/a |
CLEANROOM WHITEPAPERS AND CASE STUDIES
-

Spray drying creates stable inhalable biologic powders with controlled particle size, enabling effective lung delivery, improved stability, and scalable production for respiratory and systemic therapies.
-

Viable air monitoring is critical for environmental monitoring programs in pharmaceutical manufacturing. Explore current regulatory standards as well as the impact of the EU GMP Annex 1 revisions.
-

Integrating material characterization data with process parameters accelerates drug development, reduces empirical testing, and strengthens regulatory compliance.
-

Discover a technology platform that is revolutionizing the pre-fillable syringe market by solving the challenge of silicone sensitivity, ensuring stability for sensitive drugs.
-

Moving mRNA lipid nanoparticle encapsulation from pre-clinical work to cGMP production is often underestimated. Early process parameter definition, raw material control, and scalable mixing determine how low-risk that transition becomes.
-

Severn Trent’s smart metering program, powered by Itron’s technology, is transforming water conservation—reducing leaks by 6 million liters, cutting costs, and empowering customers to use water more wisely.
-

Modern AAV manufacturing demands precise capsid characterization to distinguish empty, partial, and full particles, as regulators now require rigorous purity and potency control for clinical safety.
-

Discover how PFAS-selective ion exchange resin offers a cost-effective alternative to traditional filtration methods. This case study details the transition to non-detectable contamination levels, showcasing the performance advantages of resin technology in securing resilient, high-quality public water supplies.
-

Gain insight into how Annex 1 reshapes aseptic process validation, as well as into risk reduction by design and why isolators are redefining modern sterile manufacturing standards.
-

The new Annex 1 revision emphasizes validation and qualification for sterile drug production. Ensure product quality and contamination control by learning about in-depth requirements for premises and equipment.
-
Learn why Spring Creek Ranch chose Echologics to survey 1.7 miles of 12-inch ductile iron pipe, utilizing the ePulse® method to assess the condition of the over 40-year-old pipes.
-

MockV® technology enables early, in-house viral clearance assessment, helping biopharma developers improve process robustness, reduce costs, and enhance safety before GMP manufacturing begins.
-

A fire in a pharmaceutical cleanroom can be contained, but for sterile manufacturers, smoke can turn a localized event into a far wider decontamination, requalification, and production-recovery challenge.
-

Does shuttle blow-fill-seal truly meet Annex 1’s stricter contamination standards? New particle burden data challenges industry assumptions and reveals what manufacturers need to know.